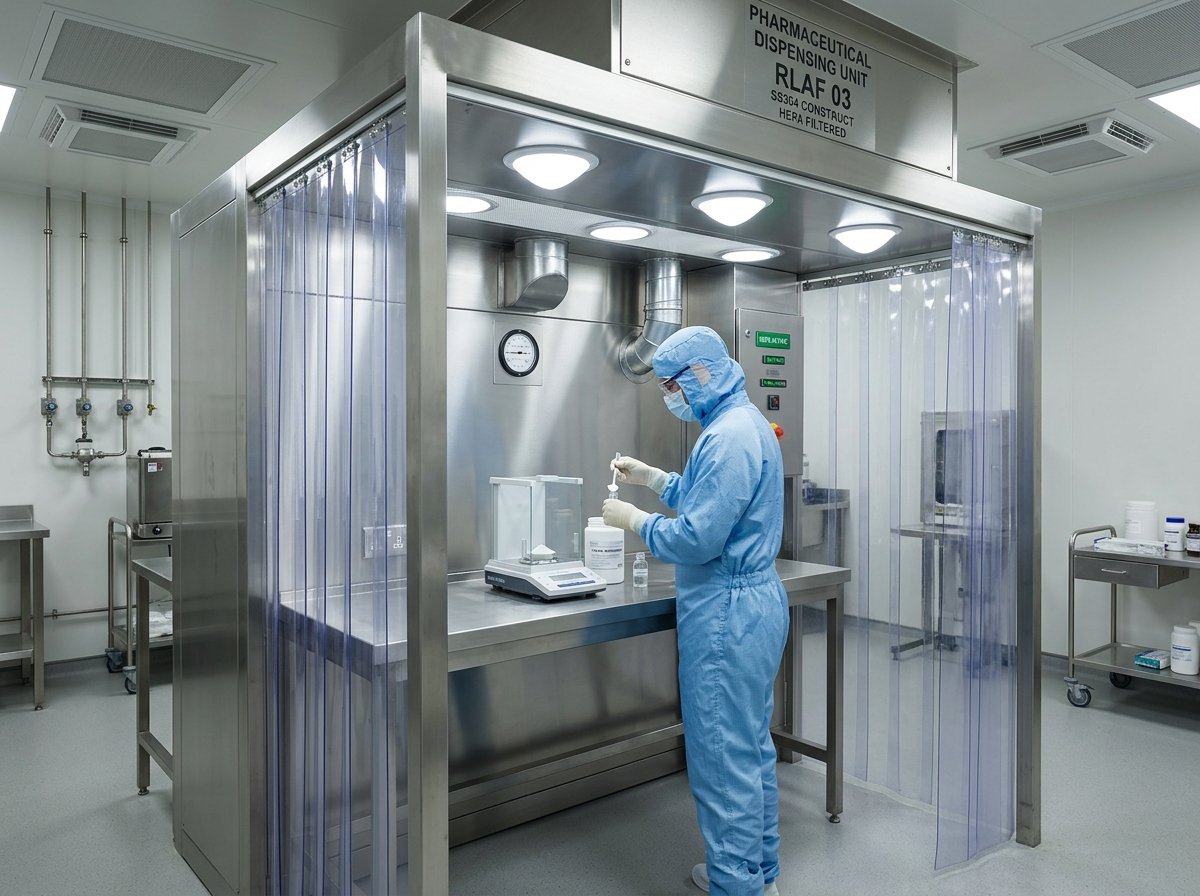
Dispensing & Sampling Downflow Booth (RLAF)
Engineered to deliver high-level containment (OEL < 10 µg/m³) during raw material powder dispensing, weighing, and sub-division. Protects operators against respiratory inhalation of potent drug dust while safeguarding the product against environmental contamination.
Engineering Overview & Fluid Dynamics
Active contamination barrier and laminar downflow principles
The Himalayan Steel Dispensing Downflow Booth operates on the Reverse Laminar Airflow (RLAF) principle. Recirculated clean air travels downward across the entire ceiling at 0.45 m/s, suppressing airborne dust clouds generated during powder scooping and weighing. Approximately 85–90% of the air is drawn into base-level extraction pre-filters, channeled through intermediate bag filters, and scrubbed through final H14 HEPA filters before returning to the ceiling. The remaining 10–15% is exhausted to create a continuous negative pressure zone within the booth, preventing powder particulates from escaping into surrounding cleanroom corridors.
Technical Engineering Specifications
Standard dimensional tolerances, electrical parameters, and air quality ratings
Standard Dimensional Matrix
Fabrication schedule comparison in Imperial and Metric standards
| Size (Feet) | Metric (MM) | Internal Chamber (W x D x H) | External Footprint (W x D x H) |
|---|---|---|---|
| 3 x 3 ft (Compact Balance) | 1000 x 1000 x 2200 mm | 900 x 900 x 2000 mm | 1100 x 1350 x 2400 mm |
| 4 x 3 ft (Standard Bench) | 1200 x 1000 x 2200 mm | 1200 x 900 x 2000 mm | 1350 x 1350 x 2400 mm |
| 5 x 4 ft (Drum & Balance) | 1500 x 1200 x 2200 mm | 1500 x 1100 x 2000 mm | 1650 x 1550 x 2400 mm |
| 6 x 4 ft (Twin Drum) | 1800 x 1200 x 2200 mm | 1800 x 1100 x 2000 mm | 1950 x 1550 x 2400 mm |
| 8 x 6 ft (Pallet Sized) | 2400 x 1800 x 2200 mm | 2400 x 1700 x 2000 mm | 2550 x 2150 x 2450 mm |
Cleanroom Construction & Architectural Design
cGMP sanitary fabrication details from our Baddi engineering works
Constructed with sandwich insulated panels and continuous GTAW sanitary corner welds, ground flush and polished for sterile detergent wipe-down.
Strategically positioned return air grilles suck generated dust away from the operator breathing zone directly at floor height.
High-efficiency backward curved motorized impellers dynamically respond to filter loading to preserve steady 0.45 m/s downflow velocity.
Ceiling HEPA filters fitted into continuous fluid gel seal troughs to eliminate particulate bypass around filter frames.
Dedicated recess designed to house heavy granite balance slabs isolated from booth floor vibrations for 4-decimal analytical weighing.
Overlapping 2 mm thick antistatic clear PVC strips suspended along front opening to define the containment boundary.
Standard Operating Protocol (cGMP SOP)
Standard operating guidelines and contamination control sequence
Step-by-Step Material Transfer Sequence
Sanitization & Wipe-Down Protocol
- Vacuum or wipe down gross powder residues using dedicated cleanroom vacuum with HEPA filter.
- Wipe all stainless walls and return grilles with approved sanitizing solvent after each batch.
- Wash primary pre-filters weekly; record filter pressure differentials daily in logbook.
Fail-Safe Interlock Protection
- Alarm sounds if airflow velocity drops below 0.35 m/s or exceeds 0.55 m/s.
- Differential pressure switches flag dirty filter warning to prevent containment failure.
Optional Engineering Customizations
Site-specific hardware adaptations
- Bag-In / Bag-Out (BIBO) safe change exhaust filter housing for highly hazardous APIs
- Flameproof (ATEX / PESO Certified) electricals for flammable solvent handling
- Integrated weighing balance display shelf and data cable pass-through glands
- Temperature-cooling coil heat exchanger for operator comfort in hot ambient rooms
- Air velocity alarm transmitter tied to central BMS monitoring system
Quality Validation Package (DQ/IQ/OQ)
Audit-ready documentation for US FDA and EU-GMP inspections
- Design Qualification (DQ) Documentation & HVAC Duct Schematics
- Installation Qualification (IQ) Protocol Checklists
- Operational Qualification (OQ) Velocity Uniformity & Pressure Profiles
- SMEPAC Surrogate Powder Containment Test Report (OEL Validation)
- DOP/PAO Filter Leak Test Certificates for Pre, Fine, and HEPA Banks
- Acoustic Noise & Air Flow Visualization Smoke Study Records
Cleanroom Design Highlights
- True 3-stage filtration hierarchy captures coarse, fine, and respirable toxic powder dust
- 10% exhaust bleed air maintains reliable negative pressure containment barrier
- Continuous Magnehelic gauge array monitors pressure differential across all filter banks
- Safe-change Bag-In / Bag-Out (BIBO) intermediate filter housing option for potent APIs
Target Pharmaceutical Applications
Explore Other Equipment Divisions
Sterile Raw Material Sampling Booth
Dedicated cleanroom raw material sampling workstation engineered for intermediate warehouse QC testing and drum thief sampling.
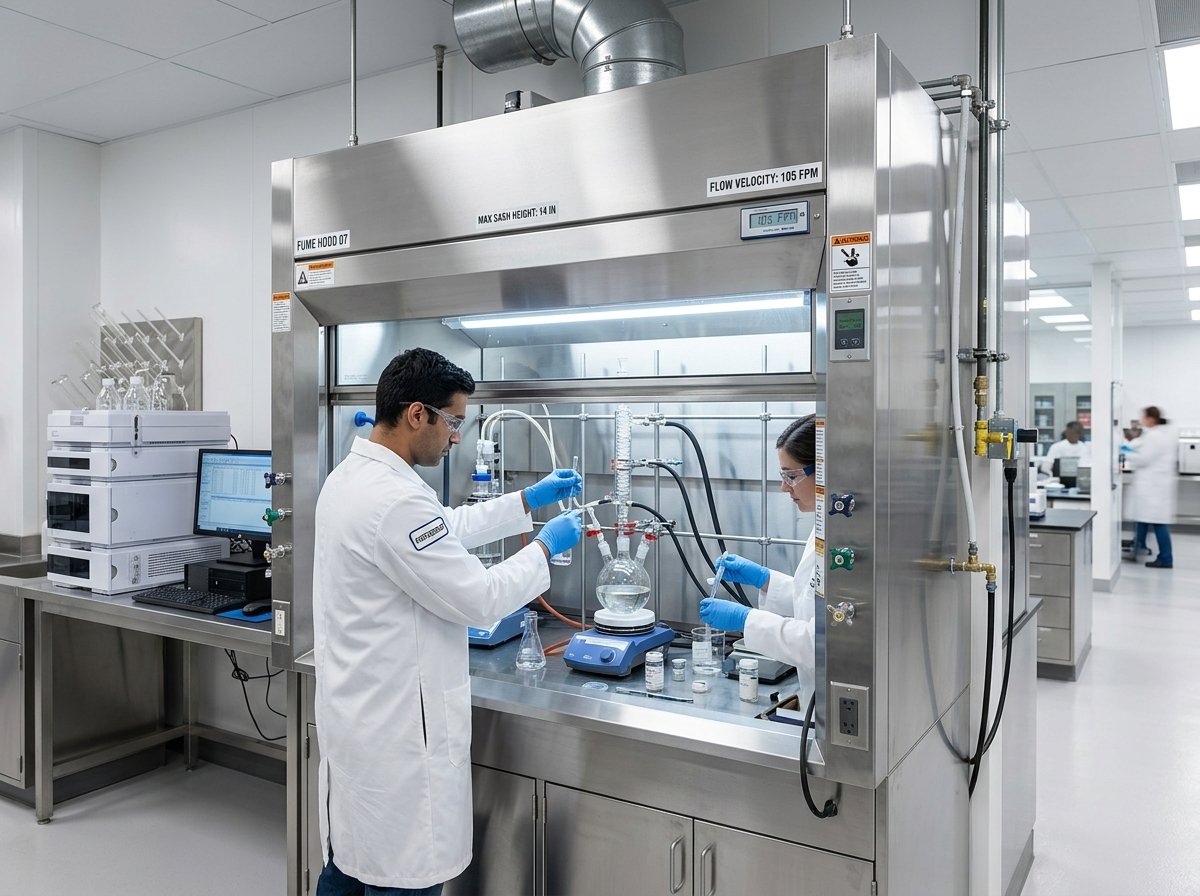
Aerodynamic Laboratory Fume Hood
High-containment aerodynamic chemical fume hood compliant with ASHRAE 110 & EN 14175 standards with bypass airflow.
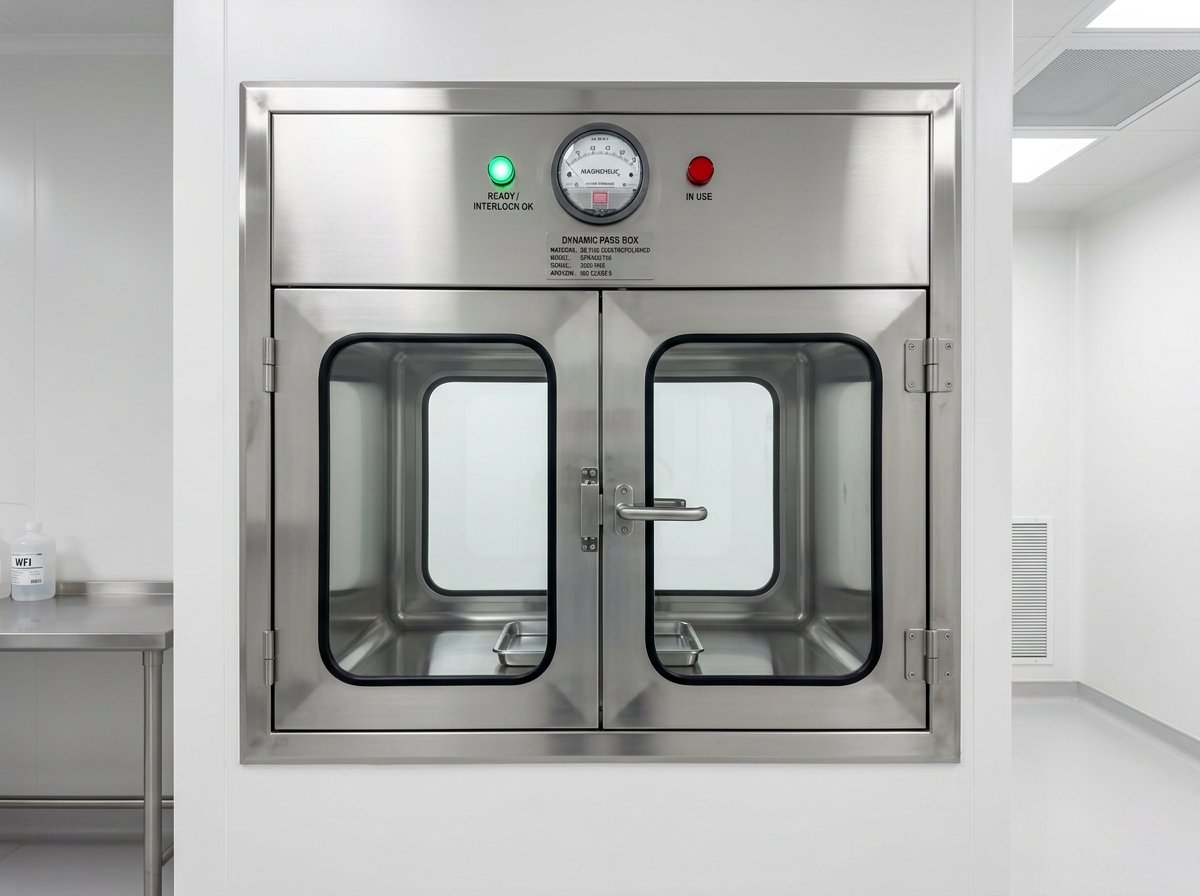
SS Dynamic Pass Box (HEPA Filtered)
Active Class 100 laminar downflow pass box with electromagnetic interlocking, Magnehelic gauge, and UV germicidal sterilization.